NewsNEWCENTER
Featured products
Contact Us
The Correct Method for Preventing Cavitation in Water-Ring Vacuum Pumps
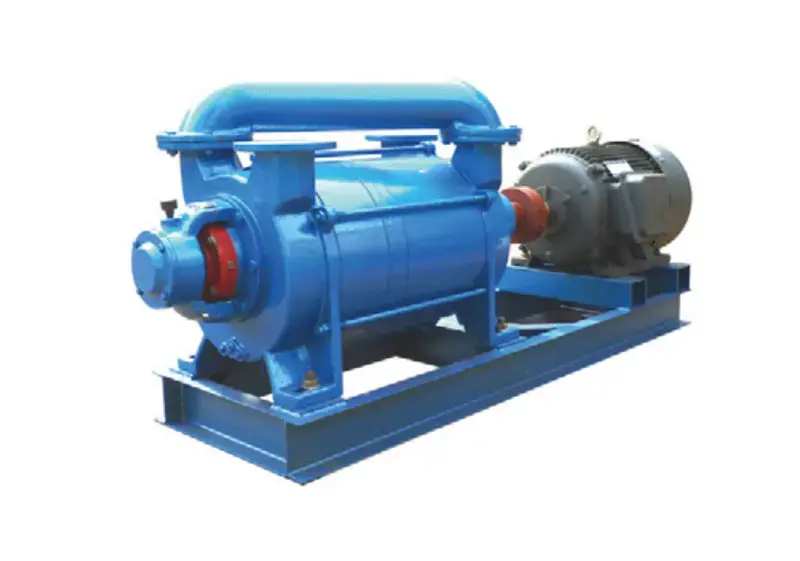
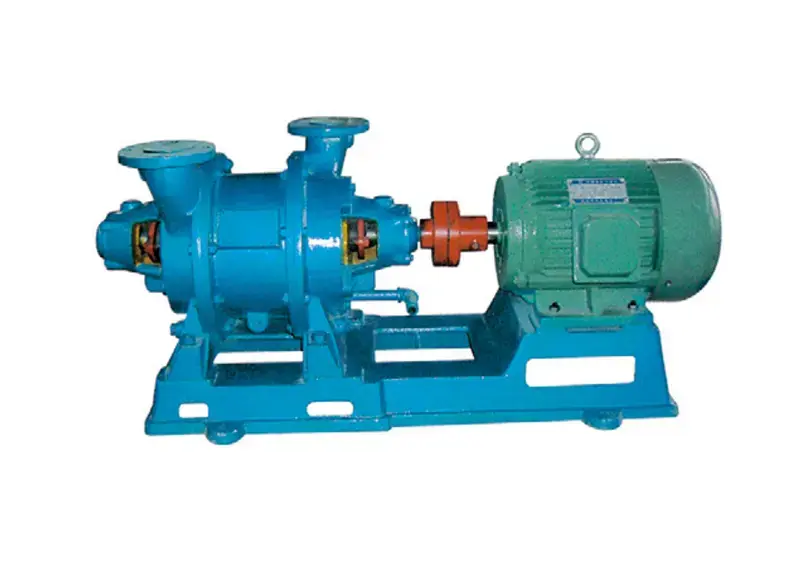
2026-08-17As water-ring vacuum pumps are widely used in many fields and offer advantages such as a long service life, higher demands are placed on their performance. To ensure optimal performance, let’s take a look at the correct methods for preventing cavitation in water-ring vacuum pumps.
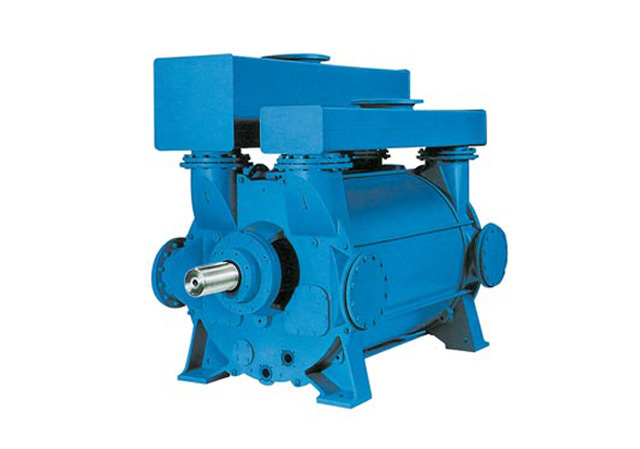
During operation of a liquid-ring vacuum pump, cavitation is an inevitable phenomenon. When the vacuum level reaches -0.093 MPa or lower, the water inside the pump chamber easily reaches its saturated vapor pressure, causing numerous bubbles to form. These bubbles rapidly burst at the discharge end due to increased pressure. The water surrounding the original bubble then quickly fills the space left by the burst bubble, causing a significant impact on the impeller and disc of the liquid ring vacuum pump, accompanied by a sharp, crackling sound. When cavitation first begins to affect the impeller and disc of a water-ring vacuum pump—primarily the impeller—it causes pitting damage, destroying the protective layer on the metal surface. As cavitation continues, honeycomb-like pits form on the impeller surface, and the depth of these pits gradually increases until the impeller blades break off due to cavitation and fluid resistance. Cavitation poses a major threat to water-ring vacuum pumps. In practical applications, many instances of reduced performance or even damage to these pumps are caused by cavitation. Given the severity of the damage caused by cavitation, an anti-cavitation protection tube device can be installed in water-ring vacuum pumps to address this issue.
The above outlines the correct methods for preventing cavitation in water-ring vacuum pumps. You can select the appropriate method based on your specific operational requirements to avoid unnecessary losses caused by improper operation. If you have any other questions, please visit our website, where we regularly update our articles. We hope this information is helpful to you.